
The three inputs to machine-hour cost
Machine-hour cost is built from three things that are each easy to look up and easy to skip:
- Depreciation — the purchase price spread across the machine's expected working life in hours. A machine you paid a lot for is not expensive to run because you paid a lot for it; it's expensive per hour only in proportion to how many hours it will give you back.
- The wear part — the consumable that has its own shorter life than the machine around it: a CO2 laser tube, a diode module, a print head, a router's spindle bit. It is priced the same way as the machine itself — replacement cost divided by its own rated hours — because it wears out on its own schedule, not the machine's.
- Electricity — what the whole machine draws from the wall (its fans, chiller and electronics, not its rated laser wattage), converted to kilowatts, multiplied by what your utility actually charges per kilowatt-hour. It is not reliably the smallest of the three: in the sample shop's rates below it is the smallest line on the CO2 laser but the middle one on both the diode and the fiber.
Two more real costs are worth naming, and worth keeping out of this number on purpose: routine maintenance and consumables — lenses, belts, filters — can be added as their own per-hour figure if you track them, but insurance and rent belong in shop overhead instead under this method. They run whether the machine is on or idle, so charging them to one machine's hourly rate overprices every job that happens to use it and underprices everything that doesn't.
How to calculate machine-hour cost
Work these three out in turn, then add them:
- Depreciation per hour = purchase price ÷ expected working life in hours. A machine bought for a fixed price and expected to run for a fixed number of hours before it's worn out or replaced.
- Wear-part cost per hour = replacement price ÷ rated hours. A CO2 tube, diode module, print head or spindle bit, each priced against its own rated life, not the machine's.
- Electricity per hour = wall draw in watts ÷ 1,000 × your electricity rate. The machine's draw in kilowatts, multiplied by what a kilowatt-hour actually costs you.
Add the three and you have a single $/hour figure for that machine. Multiply it by however long a job actually occupies the bed, and you have that job's real machine cost — a number you can put next to material and labor rather than guess at.
If you'd rather not run that arithmetic by hand: the free Laser & CNC Job Cost Calculator on our own Ardent Seller platform works out one job in your browser, though the machine-hour figure it builds covers only the first and third of the three parts above — depreciation and electricity — so the wear part is yours to add. The Laser Engraving Business Workbook computes and keeps all three for every machine in a shop, and the free Laser Settings & Material Test Log records the settings behind the burn times you will be multiplying.
Why a job costs real money even when the material is cheap
This is the reason the number matters at all. A job that ties up a machine for forty minutes carries a real cost for those forty minutes whether the blank underneath it cost ten cents or ten dollars — the machine doesn't know or care what it's cutting. Price only the material and you'll systematically underprice anything that's slow to make and overprice anything that's fast, which is exactly backwards from what a price list should do.
Getting each input honestly
The formula is simple; the discipline is in where the numbers come from.
- Rated life comes from the maker, not a guess — check the spec sheet or the listing for the tube, module, head or bit, and use the rated hours figure it gives if it publishes one. Using a round number because the real one wasn't looked up is how this whole calculation quietly drifts.
- Hours run come from a log, not an estimate. A machine you "think" has maybe five hundred hours on it could easily have a thousand — and the wear part's cost per hour is wrong in the same direction as that guess.
The sample shop's machine-hour rates
The electricity column below is computed from each machine's wall draw — 1,450 W for the CO2, 320 W for the diode, 600 W for the fiber — not from its rated laser wattage. To make the arithmetic concrete: the fictional sample shop that ships inside the Laser Engraving Business Workbook runs a CO2 laser, a diode laser and a fiber laser side by side, each with its own computed rate.
| Machine | Depreciation $/hr | Tube / module wear $/hr | Electricity $/hr | Total $/machine-hour |
|---|---|---|---|---|
| CO2 | $0.420 | $0.320 | $0.246 | $0.99 |
| Diode | $0.183 | $0.033 | $0.054 | $0.27 |
| Fiber | $0.180 | $0.035 | $0.102 | $0.32 |
The components are shown to three decimals so that each row adds to the rate beside it once rounded. The CO2 machine sits well above the other two, and the wear part is the largest single contributor to the gap between it and the diode — about 40% of that gap, with depreciation roughly a third and electricity the rest, so no one line explains it on its own. An hour on the CO2 still costs more than three and a half times what an hour on the diode does. These are figures specific to that sample shop's machines and electricity rate, not an industry number to borrow.
Common machine-hour cost mistakes
- Treating the tube or module as an occasional repair bill. A CO2 tube or diode module that gets replaced every couple of years reads, in the moment, like a one-off expense rather than a cost every job on that machine has been quietly running up all along. Spread across its rated hours, it's not occasional at all — it's baked into every hour the machine runs.
- Using a blended "shop rate" instead. A single rate that mixes labor and machine time hides which one is actually driving the cost, and it breaks the moment a second machine enters the shop with a genuinely different hourly cost of its own.
- Pricing everything off one machine's rate. A shop running both a CO2 and a diode laser — or any two machines with meaningfully different rates — that prices every job off whichever machine happens to be top of mind will overprice jobs on the cheap machine and underprice jobs on the expensive one.
- Never re-deriving the rate. Electricity rates change, tubes and modules get more or less expensive to replace, and a machine logs more hours every week. A rate computed once and never revisited drifts away from what the machine actually costs to run.
Turning a rate into a price, without redoing the math per job
Start free
A single job is easy to price by hand once: work out the machine's $/hour, multiply by the minutes on the bed, add material and labor. The free Laser & CNC Job Cost Calculator on our own Ardent Seller platform prices a single job in your browser, no signup — though the machine-hour figure it builds covers depreciation and electricity, leaving the tube or module wear for you to add. Beside it, the free Laser Settings & Material Test Log records what a material and a machine actually did together — power, speed, passes, focus and the result you got — so the settings behind a burn time are written down rather than remembered. It logs settings; it doesn't price a catalog.
Then own the rate
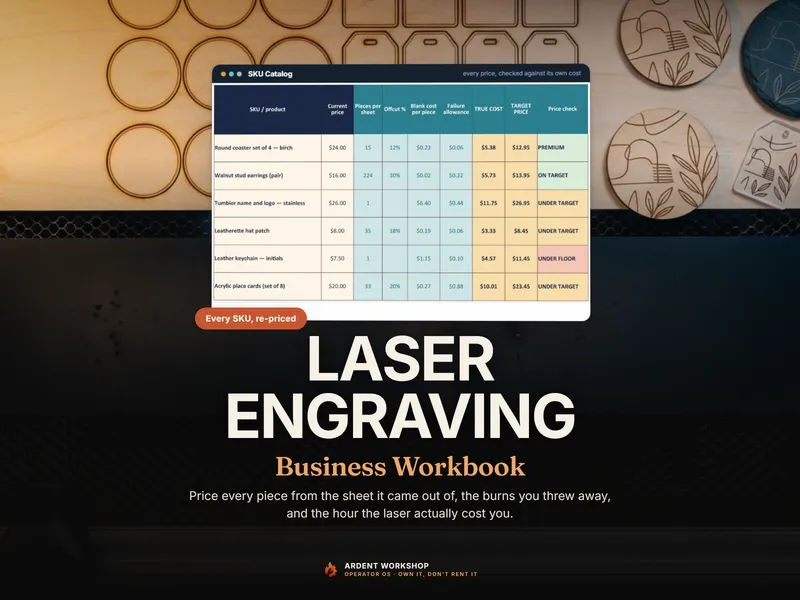
What a single-job calculator can't do is remember the rate for next time, or notice when a tube replacement or an electricity-rate change should move every price built on top of it — that's a number worth owning rather than re-deriving from scratch on every quote. The Laser Engraving Business Workbook computes each machine's $/hour once from your own setup, then folds it into every SKU's true cost so the whole catalog re-prices itself the moment a rate changes.
Related templates and concepts
Machine-hour cost is one input into cost of goods sold and, downstream of that, profit margin; on a sheet-fed machine it sits alongside material yield as the two numbers that turn a blank price into a true cost per piece. For the whole method end to end, see how to price laser-engraved products; for how the rate differs between two classes of desktop laser, see Glowforge vs xTool cost per job. Browse every tool on the templates for makers hub.
Templates that implement this
A workbook that computes your machine-hour rate for you
1 template
Set up each machine once — purchase price and expected life, tube or module cost and rated hours, watts and your electricity rate — and the workbook carries the resulting $/hour into every job and every SKU in the catalog, re-pricing the whole thing the moment a rate changes.
Frequently asked questions
- What is machine-hour cost?
- It's what it costs to run a machine for one hour: the purchase price spread across its expected working life (depreciation), plus the wear part — a laser tube, a diode module, a print head, a spindle bit — spread across its own rated hours, plus the electricity it draws at your rate. Add the three and you have a dollar-per-hour figure you can multiply by any job's time on the machine.
- How do you calculate machine-hour cost?
- Depreciation per hour = purchase price ÷ expected working life in hours. Wear-part cost per hour = the part's replacement price ÷ its rated hours. Electricity per hour = what the whole machine draws from the wall in watts — not its rated laser wattage — converted to kilowatts, × your electricity rate. Add all three for the machine's total $/hour.
- Why does machine-hour cost matter if the material is cheap?
- Because the machine's time is a real cost even when the blank is not. A job that ties up a machine for forty minutes carries that machine's $/hour rate whether the material underneath it cost ten cents or ten dollars — skip it and every job priced mostly on material looks more profitable than it is.
- What's the difference between machine-hour cost and shop rate?
- A shop rate blends labor and machine time into one number, which by construction hides which part is driving the cost and breaks the moment you add a second machine with a different rate. Machine-hour cost is the machine alone — labor is priced separately, per minute of hands-on time.
- Should insurance and rent be part of machine-hour cost?
- Not in this method. Insurance, rent and other costs that run whether or not the machine is on are treated as shop overhead, spread across your working hours generally — folding them into one machine's hourly rate overcharges every job that touches that machine and undercharges everything that doesn't.
- Where do you get the numbers for machine-hour cost?
- Rated life for the wear part comes from the manufacturer — a CO2 tube's or diode module's spec sheet, a print head's service life, a spindle bit's rated hours. Actual hours run comes from your own log, not an estimate; without a log you're guessing whether a part is due for replacement now or in a year.