"Glowforge vs xTool" reads like a shootout, but the honest question underneath it isn't which brand wins — it's how the cost-per-job math changes between a sealed-CO2 laser and a diode laser, whichever brand happens to be selling the specific unit in front of you. That math is a property of the laser class, and it's computable from numbers you already have or can look up: what the machine cost, what its wearing parts cost, what power it draws, and how long a given job actually takes on it.
Two laser classes, not two brands
The question underneath "Glowforge vs xTool" spans two kinds of desktop laser: a sealed-CO2 machine and a diode machine. The name on the lid doesn't settle which of those two you are actually comparing — you have to check the specific model's own documentation for that — so this page compares the two classes on how they turn a job into a cost. It doesn't claim a wattage, a price, a tube life, or a module life for any specific machine either company sells, and it isn't a review of either one.
Why the cost-per-job math differs, class to class
Five things separate a CO2-class machine from a diode-class machine for the purpose of cost per job, and all five are genuinely about the class — not about which brand happens to sell the specific unit on your bench:
- The wear part. A sealed CO2 laser fires through a tube that's a consumable with a rated life — it's expected to degrade and eventually be replaced, so its cost belongs in your hourly rate, spread over the hours it's rated to last. A diode module is priced the same way, against its own replacement cost and its own rated hours; the two numbers are simply different, which is what moves this line between the classes rather than removing it.
- Cut speed and passes. Whichever machine takes longer to finish a given job — because the material needs more passes, or a slower feed rate to cut cleanly — ties up more machine-minutes for that piece. Machine-minutes are a straight multiplier against your machine-hour rate, so a slower job costs more even at an identical rate, and a faster one costs less even at a higher rate.
- Power draw. What the machine pulls from the wall — not its rated laser wattage — sets the electricity line of your machine-hour rate. It also often moves the speed side of the job at the same time, which is exactly why the two can't be judged separately — more power can mean a higher electricity cost and fewer machine-minutes on the same job, and the net effect only shows up once you run both through the formula.
- What the class can cut at all. The two beam types don't interact with every material the same way, so which materials are even eligible for a job depends on the class before it depends on the brand. That decides which blanks — and which blank costs and failure rates — enter your math in the first place. A material one class can't touch isn't a cost comparison; it's a different question.
- Capital cost spread over expected life hours. A machine's purchase price only matters per job once it's divided by how many hours you actually expect to run it. A pricier machine you run constantly can carry a lower cost per hour than a cheaper one that mostly sits idle — the purchase price alone never tells you which.
The machine-hour rate: the number underneath every job
Before you can price a single job, you need one number: what an hour on that specific machine actually costs you to run — its machine-hour cost. It is three parts. Work them out in turn, then add them:
- Depreciation per hour — the purchase price divided by the machine's expected life in hours.
- Wear-part cost per hour — the tube's or module's replacement cost divided by its own rated hours.
- Electricity per hour — the wall draw in watts (the whole machine, not the rated laser wattage) divided by 1,000, then multiplied by your electricity rate per kilowatt-hour.
The electricity lines below come from each machine's wall draw — 1,450 W for the CO2 and 320 W for the diode in that sample shop — not from its rated laser wattage, which is why a 20 W diode machine is not a 20 W load. And whichever class you run, the settings that produced a good burn are worth keeping: the free Laser Settings & Material Test Log is a pre-filled place to write them down.
Each machine you own gets its own rate. A CO2 machine and a diode machine won't share a wear-part line at all, since the tube and the module are priced and rated differently, and they may not share a power line either.
Job cost: what a specific piece actually takes
The machine-hour rate feeds into the number that actually prices a job. Job cost is the sum of five lines:
- The blank cost per piece — what one piece of material costs once the sheet is divided by how many pieces it really yields.
- The machine cost — the machine minutes divided by 60, multiplied by that machine's own machine-hour rate.
- The labor cost — the hands-on minutes divided by 60, multiplied by a loaded rate: your hourly pay plus your shop overhead spread across the hours you actually work.
- A waste allowance — what the pieces that fail cost the ones that survive.
- Packaging and fees — what goes in the box, plus the sale channel's flat per-order charge. Its percentage cut is not a cost you add: it comes off the price, so the price has to be solved for a margin that already accounts for it.
Run the same job through both machines' numbers, and the machine with the lower machine-hour rate doesn't automatically win. If it also takes meaningfully longer on that specific material, the extra minutes can erase the advantage the lower rate gave it. There's no shortcut around computing both sides.
Why the "cheaper" machine can lose on a specific job
A lower machine-hour rate isn't the same thing as a lower job cost, because the rate is only half the multiplication. A machine that costs less to run for an hour can still cost more to run a specific job if it needs more passes, a slower feed, or more setup to get a clean result on that material — the extra minutes multiply against the rate the same way the material and labor lines do. Rank two machines by their machine-hour rate alone and you're only telling half the story; rank them by job cost on the specific piece you're actually pricing, and the order can flip.
What one sample shop's numbers looked like
The Laser Engraving Business Workbook ships with a fictional sample shop already filled in, so you can see the math work before entering your own numbers. Run through the formula above, that shop's CO2 machine priced out to about $0.99 a machine-hour and its diode machine to about $0.27 a machine-hour.
| Sample shop's machine | Depreciation $/hr | Tube / module wear $/hr | Electricity $/hr | Total $/machine-hour |
|---|---|---|---|---|
| CO2 | $0.420 | $0.320 | $0.246 | $0.99 |
| Diode | $0.183 | $0.033 | $0.054 | $0.27 |
The wear-part line was the largest single piece of the gap between them, about 40% of it: the CO2 tube contributed about $0.32 an hour of that $0.99, against roughly $0.033 an hour for the diode module. Depreciation accounted for about a third of the gap and electricity for the rest, so the wear part moved it most but did not make it on its own.
Those are one fictional shop's numbers, not a claim about what either brand's machines cost to run. A different purchase price, a different electricity rate, or a different expected life changes every term in the formula. They're published here only to show what plugging real numbers into the math looks like.
Get the number for your own shop
Start free
The free Laser & CNC Job Cost Calculator on our own Ardent Seller platform prices one job right in your browser — no email, no signup — so you can see a job cost before deciding whether to go further. Its machine-hour figure covers depreciation and electricity, so add the tube or module wear yourself. Pair it with the free Laser Settings & Material Test Log to keep a record of the setting and the result you tested, material by material and machine by machine. If you want the whole costing method worked through step by step, see how to price laser-engraved products.
Then price the whole catalog
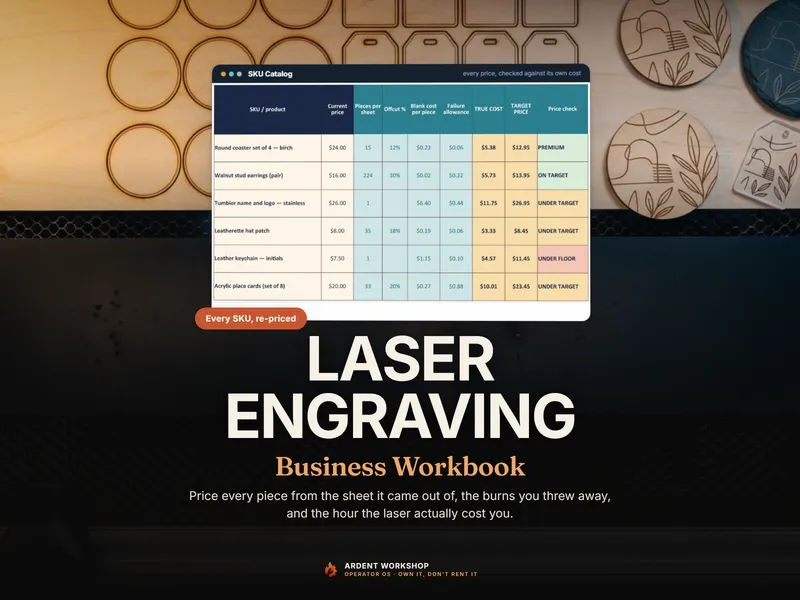
The Laser Engraving Business Workbook computes a machine-hour rate for every laser in your shop from its own purchase cost, wear part, and electricity rate, then re-prices your entire SKU catalog against it — so the moment a tube, a diode module, or your electricity rate changes, you see exactly which prices fall under target instead of re-running the arithmetic by hand for every item.
Frequently asked questions
- Is a CO2 laser or a diode laser cheaper to run?
- It depends on your own machine-hour rate and the specific job — there's no fixed answer across the two classes. A CO2 tube and a diode module are priced and rated differently, so one class doesn't universally win on the wear-part line, and cut speed on a given material can shift the balance either way. Compute the machine-hour rate for your specific machine, then price the job through it, rather than assuming either class is cheaper in general.
- Why does the CO2 tube matter so much for cost per job?
- Because it's a wearing consumable with a rated life, not a one-time purchase. Every hour you run a sealed-CO2 laser uses up part of that tube's life, so its replacement cost belongs in your hourly rate the same way depreciation does — divide what the tube costs by the hours it's rated to last, and that's the hourly line it adds. Skip that line and every job priced on that machine is quietly undercosted.
- Does higher wattage always mean a higher cost per job?
- No — wattage only sets the electricity line of the machine-hour rate directly, and that line is one of three, sized against depreciation and wear; how large a share it takes depends on the specific machine. What actually decides the outcome is whether the higher power also finishes the job faster: fewer machine-minutes at a slightly higher electricity cost can still come out cheaper than more machine-minutes at a lower one. You have to run both sides of the formula to know which way a specific job goes.
- Can I compare a CO2 laser's cost per job to a diode laser's if only one can cut the material?
- Not as a cost comparison — that's a capability question first. Cost per job only makes sense to compare across two machines that can both actually produce the piece; if a material is off the table for one class entirely, there's no rate at which the other one is "more expensive," because the alternative doesn't exist. Compare cost only across the jobs both machines can genuinely make.
- How do I include a laser tube or diode module replacement in my price?
- Divide the part's replacement cost by the number of hours it's rated to last, and add that figure to your machine-hour rate alongside depreciation and electricity. It's the same treatment a workshop gives any wearing part — a drill bit, a blade, a filter — priced as an hourly cost instead of a one-time purchase, so it's already inside every job's price instead of showing up as a surprise the day the part fails.